Plum brandy is one of the most important fruit brandies in Serbia, where are we from, and is widely regarded as a traditional homemade spirit. It is produced from ripe, healthy, and technologically suitable plum fruits, while the quality of the final product depends on the raw material, properly managed fermentation, careful distillation, and appropriate aging.
The most commonly used variety is Požegača — accounting for around 50% — while other widely used plum varieties for rakija production include Crvena Ranka, Metlaš, Trnovača, Moravka, Piskavac, white plums, Dženerika, Petrovka, and Mirisavka.
The technology of processing plums into rakija includes the following steps:
Harvesting the plums
Collecting and transporting the plums to fermentation vessels
Crushing the plums and separating the pits
Alcoholic fermentation of the plum mash
Distillation of the fermented plum mash
Aging and finalizing the šljivovica
For the production of high-quality šljivovica, fully ripe, healthy, and undamaged fruits should be used. Rotten, moldy, or dirty fruits must be removed, as they have a negative effect on the fermentation process and on the aroma of the rakija.
After harvesting, the fruit should be transported to the processing site as soon as possible. It is recommended to organize processing quickly and evenly in order to avoid fruit spoilage and the development of undesirable microorganisms.
Crushing the plums allows fermentation to begin faster and proceed more evenly. It is advisable to remove the pits, or at least to keep them intact, because broken pits may lead to a stronger stone-like aroma, bitterness, and lower distillate quality.
The crushed mass is placed into fermentation vessels, which should be filled to approximately 4/5 of their capacity. The vessels should be closed in a way that allows carbon dioxide to escape while limiting air access.
For proper fermentation, the most important factors are temperature, sugar content in the fruit, the degree of crushing, and the use of suitable yeast. Selected yeasts should be added according to the manufacturer’s instructions, as they contribute to a more stable and reliable fermentation process. The recommended fermentation temperature is approximately 16–20 °C, while the duration of fermentation depends on the conditions and may last from about one to four weeks.
Distillation is the stage in which alcohol and aromatic compounds are separated from the fermented mash, while undesirable volatile and less volatile components are also removed. In practice, double distillation is most commonly used for šljivovica: first, a low-strength distillate is produced, commonly referred to as soft rakija, and then it is distilled again to obtain the final distillate, known as prepek.
This method usually produces a cleaner, more balanced, and higher-quality distillate than single distillation, because it allows for more precise separation of fractions.
The soft distillate is obtained through the first distillation of the fermented mash. The fermented mash is poured into the still, taking care not to overfill the boiler and to prevent boiling over or the transfer of solid particles into the vapor pipe. Heating should be gradual and even.
The purpose of the first distillation is not to produce finished drinking rakija, but to extract alcohol and aromatic compounds from the mash and concentrate them into the so-called soft rakija, which will serve as the raw material for the second distillation.
During the first distillation, a smaller portion of the initial fraction is usually separated, after which the main flow of distillate is collected, while the weaker final part is separated as the tail fraction. In domestic technological literature on šljivovica, it is often stated that the first distillation produces a soft distillate of approximately 25–30% vol., with the beginning and end of the flow separated according to the strength of the distillate and its sensory properties.
These figures should be understood as a practical guideline rather than an absolute rule, since the actual cuts depend on the plum variety, the quality of the mash, the type of still, and the heating regime.
The final distillate, or prepek, is obtained through the second distillation of the soft distillate. This is the most important distillation stage for the quality of the rakija, because this is where the fractions are separated most precisely: heads, heart, and tails.
Unlike the first distillation, where the goal is to concentrate alcohol from the mash, the purpose of the second distillation is to separate the middle and highest-quality part of the distillate — the part with the best balance between alcohol and typical fruity aroma.
The second distillation should be carried out more slowly and carefully than the first. A slower distillate flow makes it easier to detect the transitions between fractions and allows for better quality control.
Scientific and technical studies on fruit distillates indicate that the composition of volatile compounds changes during distillation: at the beginning, more highly volatile compounds are released; in the middle flow, ethanol and desirable aromas dominate; while toward the end, the proportion of heavier components increases, which can negatively affect the purity of taste. This is why the distillate is divided into heads, heart, and tails.
The heads are the initial fraction of distillation. They contain a higher proportion of highly volatile compounds, such as acetaldehyde, ethyl acetate, and other compounds with a sharp, penetrating, and “green” aroma. For this reason, the heads are not used as the main product, but are separated at the beginning of the second distillation.
In practice, the separation of heads is determined by a combination of smell, taste, working temperature, flow speed, and distillate strength — not by a single fixed number.
It is important to note that, in fruit distillates, the topic of methanol is often oversimplified. Scientific reviews indicate that methanol in fruit brandies is primarily formed from pectin during fruit processing and fermentation, and its distribution during distillation is not the same as the distribution of typical “head” compounds.
This means that quality and safety do not depend only on discarding the first few milliliters, but much more on the quality of the raw material, keeping the pits intact, hygiene, proper fermentation, and careful management of the entire distillation process.
The heart is the middle and most valuable fraction of distillation. This is the part that is kept as the base of the future rakija, because it contains the largest portion of ethanol together with desirable fruity aromas. A properly separated heart gives rakija fullness, drinkability, and a clean plum aroma.
The collection of the heart begins when the harshness of the heads disappears, and it ends when heavier, oilier, and rougher tones start to appear in the distillate, indicating the transition into the tails.
During the second distillation, the heart is not determined by an alcoholmeter alone. Alcohol strength is a useful guideline, but in practice, sensory control is equally important.
An experienced producer recognizes the transition from heads to heart by the softening of sharp notes and the appearance of a cleaner, fruitier aroma. The transition from heart to tails is recognized by a decline in purity, the appearance of heavier notes, and a “tail-like” finish. Scientific studies on the fractions of fruit distillates confirm that the composition of the distillate changes gradually, not suddenly, which is why cuts are always a technological decision rather than a single fixed boundary.
The tails are the final fraction of distillation. In this fraction, the proportion of heavier and less desirable components increases, resulting in a cloudier, rougher, and less clean aromatic profile. For this reason, the tails are separated from the heart as soon as heavier aromas begin to dominate and when the strength of the distillate drops significantly.
In traditional distillation practice, tails are often collected separately and later processed again, but they are not mixed with the high-quality heart if the goal is to produce good šljivovica.
High-quality plum rakija can only be obtained if all steps are carried out properly: selecting healthy and ripe fruit, proper crushing, carefully managed fermentation, controlled distillation, and appropriate aging. It is the harmony between these stages that determines the aroma, fullness, and overall quality of the final product.
Fresh distillate may rest briefly in neutral vessels for stabilization, while oak barrels are most commonly used for aging and refinement. During aging, the rakija develops a more complex aroma, a softer taste, and its characteristic color.
After maturation, the rakija is diluted to the desired strength, most commonly around 40–45% vol., and then filled into suitable packaging.
Fruit brandy obtained by distilling fermented mash made from a specific pear variety, most commonly the Williams pear type. Williams pear brandy is characterized by a very pronounced and recognizable fruit aroma, but at the same time it is technologically sensitive. Williams pear fruits contain a relatively high amount of aromatic compounds, while their total acidity is low, so in production it is necessary to carefully manage mash preparation, fermentation, and distillation in order to preserve the typical varietal aroma and avoid quality losses. The key factors are fruit quality, adjustment of fermentation conditions, yeast selection, and proper fraction cuts during distillation.
Selection of raw material and harvesting
For the production of high-quality pear brandy, ripe, healthy, and undamaged fruits are used. Harvesting is most often done by hand, as this reduces bruising and juice losses, while also allowing poor-quality fruits to be roughly separated immediately. Fruits that are insufficiently ripe do not provide a full aroma, while rotten, moldy, and heavily damaged fruits spoil the mash and increase the risk of undesirable microflora. In practice, Williams pears are often left to ripen further after harvesting, until the fruit softens, turns yellow, and becomes technologically suitable for processing. Green fruits are left to ripen, while rotten areas, stems, and parts that may compromise quality are removed.
In pear brandy production, the ripening stage is particularly important because the most characteristic aromatic profile develops only in fully ripe fruits. The production of a high-quality distillate begins with the fermentation of fully ripe fruits, precisely in order to preserve and transfer the varietal aroma into the brandy as much as possible.
Washing, cleaning, and fruit preparation
After harvesting and ripening, the fruits should be washed and dried in order to remove mechanical impurities and possible microbiological contaminants from their surface. This is followed by inspection and cleaning: rotten areas, stems, and all parts that could negatively affect fermentation or introduce foreign flavors into the distillate are removed. Seeds are also removed when possible, which is justified as a technological measure because it reduces the risk of harsh and undesirable tones in the distillate.
Unlike plums, with pear brandy there is not always an insistence on coarse crushing immediately after receiving the fruit, because after ripening the fruit often softens sufficiently on its own. However, the goal is ultimately to obtain a uniform fruit mass suitable for fermentation, because evenly crushed mash enables more stable yeast activity and better release of aromatic compounds.
Crushing the fruit and forming the mash
Crushing Williams pear fruits is carried out only when necessary, that is, when the fruits have not softened sufficiently during ripening. If the fruits are well ripened, pressing and homogenization during the filling of the fermentation vessel are often sufficient. If the mass is too thick, in practice a small amount of water is sometimes added to make the mash more suitable for fermentation and later heating in the still, but this should be done very carefully, because excessive dilution reduces yield and weakens the varietal character of the brandy.
With pear brandy, it is important that the mash is neither too thick nor too diluted. A mass that is too thick makes uniform fermentation more difficult and increases the risk of scorching during distillation, while too much water reduces the concentration of dissolved aromas and sugars. Therefore, properly prepared mash is regarded as a homogeneous, easily fermentable fruit mass with preserved natural aromatic potential.
Mash acidity, yeast, and nutrients
One of the most important characteristics of pear brandy production is the naturally low acidity of the fruit, which is why, when necessary, the acidity of the mash is corrected to a technologically favorable pH, in a controlled manner, with measurement and the use of appropriate oenological agents.
The use of selected yeast is also very useful for pear brandy, because spontaneous fermentation often gives uneven results and can lead to aroma loss. In the scientific work of Professor Ninoslav Nikićević, fermentation variants with the addition of active yeast and mineral salts were part of the research precisely because fermentation significantly affects the chemical composition and sensory properties of pear brandy. Along with yeast, appropriate yeast nutrients may also be added when necessary, but again according to the technological recommendation of the product, not by guesswork.
Alcoholic fermentation
The prepared mash is poured into fermentation vessels that are not filled to the top, leaving free space for foaming and the release of carbon dioxide. The vessel should be closed in such a way that CO₂ can escape, while air access remains limited. This reduces the risk of oxidation and acetic spoilage.
In pear brandy production, fermentation must not be too vigorous. This is one of the most important technological differences compared to some other fruit brandies. Fermentation of fully ripe fruits should be carried out slowly and at a low temperature, optimally around 18 °C, in order to preserve the valuable aromatic compounds as well as possible. The mash should be kept uniform, with daily stirring.
Fermentation is considered complete when practically all fermentable sugar has been consumed, when intensive gas release stops, and when the sharp, active fermentative smell disappears from a sensory point of view. In technology, however, it is much more reliable to rely on sugar measurement and monitoring the course of fermentation than on smell alone. Well-managed fermentation of pear brandy produces a clean, aromatic, and stable fermented mash that must immediately continue to further processing.
Time between the end of fermentation and distillation
In pear brandy production, it is especially important that distillation be carried out very soon after fermentation is complete. This is not a casual recommendation, but one of the most important technological measures. According to professional sources, distillation of the fermented crushed fruit should be carried out within 48 hours after the end of fermentation, so that the content of harmful and harsh components does not increase and so that the secondary aroma formed during fermentation is not lost. If this is not possible, the barrel must be hermetically sealed until distillation.
First distillation, obtaining the soft distillate
The first distillation of fermented Williams pear mash has the task of separating alcohol and aromatic compounds from the pomace and transferring them into the so-called soft distillate or raw soft brandy. The mash is not poured into the still to the top, but only to about 2/3 of its volume, which reduces the risk of boiling over and carrying solid parts into the steam pipe. With fruit pomace, and especially thick pear pomace, it is desirable for the still to have an agitator or at least protection against scorching. In the scientific work on pear brandy, it is stated that it is useful for the still to be equipped with an agitator or at least a copper grate in order to prevent the contents from scorching.
For pear brandy, one specific detail is important, namely the recommendation that the heads should not be separated during the first distillation, in order to preserve more varietal aromas, and that the cut should be made between the soft distillate and the weak final fraction. In Nikićević’s work, it is stated that during the distillation of fermented mash for obtaining raw soft brandy, the heads are not separated, while the middle fraction is separated from the weak fraction when the average strength of the contents falls to around 20% vol. Your text mentions that the soft brandy after the first distillation has around 20–25% vol., while in some other variants for fruit brandies a range of around 20–30% vol. is stated; the differences depend on the raw material, the apparatus, and process management.
Second distillation, double distillation
The second distillation, or double distillation, is the most important stage for the final quality of pear brandy. Raw soft brandy from previous batches is placed in the still, and distillation is carried out more carefully and more slowly than during the first distillation. Your text correctly emphasizes that the second distillation is performed more gently and with mandatory separation of fractions. Scientific papers also show that fraction cuts in pear brandy are decisive for sensory finesse and that the middle fraction must be carefully separated from the heads and tails.
Heads
The heads are the initial fraction of the second distillation. They contain more easily volatile compounds, especially acetaldehyde and ethyl acetate, which give sharpness to the aroma and harshness to the taste. In Nikićević’s work, it is stated that during the redistillation of pear brandy, the heads are separated in an amount of 0.5–1.5% of the volume of raw soft brandy being redistilled, with a smaller cut being possible when the starting raw material was of excellent quality. Your text gives a similar recommendation of 1–1.5%, which falls within this range. However, in a well-written professional text, it should be added that the final cut is also determined sensorially, and not only by percentage.
Heart
The middle fraction, or heart, represents the main and most valuable part of the double distillation. In pear brandy, the heart must retain the typical, clean, and intense varietal pear aroma. Scientific papers indicate that the middle fraction should not be cut too low, because this leads to a loss of authentic aroma and fullness. A 2005 paper states that the achieved strength of the middle fraction should not be lower than 45% vol., while 50–55% vol. is given as a favorable range for separating the heart, and sometimes even up to 60% vol. is desirable. Your text states that the middle fraction should be 55–58% vol., which is a completely usable practical range if combined with smell and taste as the main criteria.
Tails
The tails are the final fraction of distillation and contain more heavy, harsh, and less desirable components. In pear brandy production, the transition from heart to tails must be made in time, before the distillate begins to lose purity and show cloudiness, bland-sour, or bitter tones. Your text observes exactly this well: the cut to tails should be made before the distillate becomes cloudy and before undesirable taste impressions appear. After that, the tails are separated until the alcohol is almost completely exhausted from the still.
Single and double distillation
Although pear brandy is traditionally often produced by double distillation in a classic copper still, your text correctly also mentions more modern apparatuses that make it possible to obtain a distillate of appropriate strength in a single cycle. Such units have elements for strengthening and purifying vapors, such as a short column and a dephlegmator. However, regardless of the construction of the apparatus, the basic technological goal remains the same: to preserve the varietal aroma of pear brandy and properly separate undesirable fractions. More recent studies on the distillation of fruit brandies confirm that the heating regime and reflux significantly affect the composition of the distillate, so in pear brandy production, process speed and energy control play a major role in final quality.
Stabilization, aging, and finalization
Unlike plum brandy, pear brandy is most often described in professional sources as a brandy consumed colorless, after stabilization in glass or stainless steel vessels. A 2016 paper states that pear brandy “never matures in a barrel” because the primary aromatic components do not combine well with secondary components from wood. A similar point is made in an older paper from 2005: new pear brandy is sharp and disharmonious, so it requires physical stabilization and gradual maturation in glass or chrome-nickel vessels for at least about 60 days, after which it is diluted to a final strength of 40–45% vol.
Your text also mentions the possibility of storage in an oak barrel. This is not entirely incorrect if referring to a special product style, but for classic pear brandy, the better and more professionally grounded recommendation is that it should be aged and stabilized in neutral vessels, so that it remains colorless and preserves its distinctly fruity profile. Dilution is carried out gradually, in several stages, with distilled or demineralized water, not abruptly immediately after distillation is complete. This is also well emphasized in your text and is worth keeping.
Conclusion
The production of pear brandy requires more technological precision than it may seem at first glance. It is not enough simply to process pears into brandy; it is essential to use fully ripe and healthy fruits, to correct mash acidity when necessary, to conduct fermentation slowly, in a controlled manner and at around 18 °C, to carry out distillation immediately after fermentation is complete, and to carefully separate the heads, heart, and tails during the second distillation. Only then is true pear brandy obtained: colorless, clean, highly aromatic, and varietally recognizable.
Apricot brandy is a fruit brandy obtained by distilling fermented apricot mash made from fresh fruit. The quality of apricot brandy depends on the choice of raw material, the degree of fruit ripeness, properly managed fermentation, careful distillation, and appropriate aging. The characteristic aroma and fragrance of this brandy come from the apricot fruit itself, which is why all technological steps must be carried out carefully and under control.
The technological process for producing apricot brandy includes the following operations:
- harvesting the fruit when ripe or slightly overripe
- crushing the fruit and, if possible, removing the pits
- alcoholic fermentation of the mash in closed vessels
- distillation of the fermented mash
- aging and finalization of the brandy
For the production of high-quality apricot brandy, fully ripe, healthy, and undamaged fruit is used. Fruit that is partially overripe can also give very good results, as at that stage it has a more pronounced aroma and greater technological suitability for processing. Rotten, moldy, and spoiled fruit must be removed, as it negatively affects both the course of fermentation and the quality of the future distillate. Apricots are crushed when necessary. If the fruit is sufficiently ripe or overripe, it often becomes partially crushed under its own weight during filling of the fermentation vessels. When crushing is done mechanically, the equipment used must not break the pits.
It is desirable to remove the pits completely, or at least partially, because prolonged contact with the mash can lead to bitter notes and almond-like aromas, which negatively affect the quality of the brandy. If the pits remain in the mash, distillation should be carried out immediately after fermentation is complete.
The crushed mass is placed into fermentation vessels, which are filled to approximately 70–80% of their capacity in order to leave room for the release of carbon dioxide and the rising of the mash during fermentation. The vessels should be closed in such a way that carbon dioxide can escape, while access to air is limited. During fermentation, occasional stirring of the mash is recommended, especially if pits or solid parts of the fruit remain in it.
Alcoholic fermentation is a biochemical process in which yeast breaks down the sugars from the fruit and converts them into ethanol and carbon dioxide. For successful fermentation, important factors include temperature, raw material composition, vessel hygiene, the presence of suitable yeast, and properly adjusted acidity of the mash. The mash should be kept in the shade at a moderate temperature, and it is preferable that the fermentation temperature does not exceed approximately 18–20 °C. Under such conditions, fermentation usually lasts about 10 to 14 days, although its duration depends on the degree of fruit ripeness and the overall process conditions.
Before fermentation begins, the acidity of the mash may be adjusted in order to prevent the development of undesirable microorganisms and to create more favorable conditions for yeast activity. This measure is carried out carefully and in accordance with technological requirements, because proper acidity contributes to a more stable and reliable fermentation process. The distillation of fermented mash is one of the most important stages in the production of apricot brandy, since the purity, aroma, and fullness of the future brandy largely depend on it. Copper stills are the most suitable for producing high-quality brandy, as copper has a beneficial effect on the distillation process and contributes to the formation of a cleaner aromatic profile in the distillate. The boiler is filled to approximately two-thirds of its capacity in order to prevent boiling over and the carryover of solid particles into the vapor pipe.
For apricot brandy, double distillation is most commonly applied. In the first distillation of the fermented mash, low wines are obtained, meaning a raw distillate containing approximately 25–30% alcohol by volume. The goal of the first distillation is not to obtain a finished drinking brandy, but to separate the alcohol and aromatic compounds from the mash and transfer them into the raw distillate. During the first distillation, the flow of the distillate is monitored, and the weaker final portion is separated as the tails fraction. Through the second distillation of the low wines, a cleaner and higher-quality distillate is obtained. This is the most important stage in shaping the final quality of the brandy, because it is then that the fractions are separated more precisely: heads, heart, and tails. The heads are the initial fraction of the distillation and contain a higher share of volatile compounds that give a sharper and less pleasant aroma. That is why they are separated at the beginning of the second distillation.
The heart is the middle and highest-quality fraction, forming the foundation of the future brandy. It contains the most favorable balance of ethanol and desirable aromatic compounds characteristic of apricots. A properly separated heart gives the brandy fullness, harmony, and a typical fruity aroma.
The tails are the final fraction of the distillation and contain a higher proportion of heavier and less desirable compounds, which is why they are separated from the heart as soon as a drop in distillate quality is noticed, the aroma changes, or the alcohol strength decreases significantly.
The apricot brandy obtained through double distillation is usually collected at around 60–70% alcohol by volume. Fresh distillate is typically sharper and less balanced in taste, which is why it is not ready for use immediately after distillation.
After distillation, apricot brandy is subjected to aging, that is, maturation. This process lasts at least several months, while for shorter stabilization the distillate may be stored in glass or stainless steel containers. In such vessels, the brandy remains colorless and retains its pronounced fruit character. If aging takes place in oak barrels, the brandy develops a golden-yellow color, a smoother taste, and a more complex aroma. The choice of aging vessel depends on whether the goal is to emphasize the fresh, fruity character of apricots or a more refined flavor influenced by wood.
Finalization represents the final preparation of the brandy for use. It includes reducing the alcohol strength to the desired level, most often to 40–50% alcohol by volume, by adding distilled or demineralized water, as well as stabilizing the brandy and preparing it for bottling. High-quality apricot brandy can only be obtained if all technological steps are properly carried out: the selection of healthy and ripe fruit, careful crushing, controlled fermentation, professionally managed double distillation, and proper aging. Only the proper coordination of all these stages makes it possible to obtain a brandy with a pronounced fruity aroma, harmonious taste, and high overall quality.
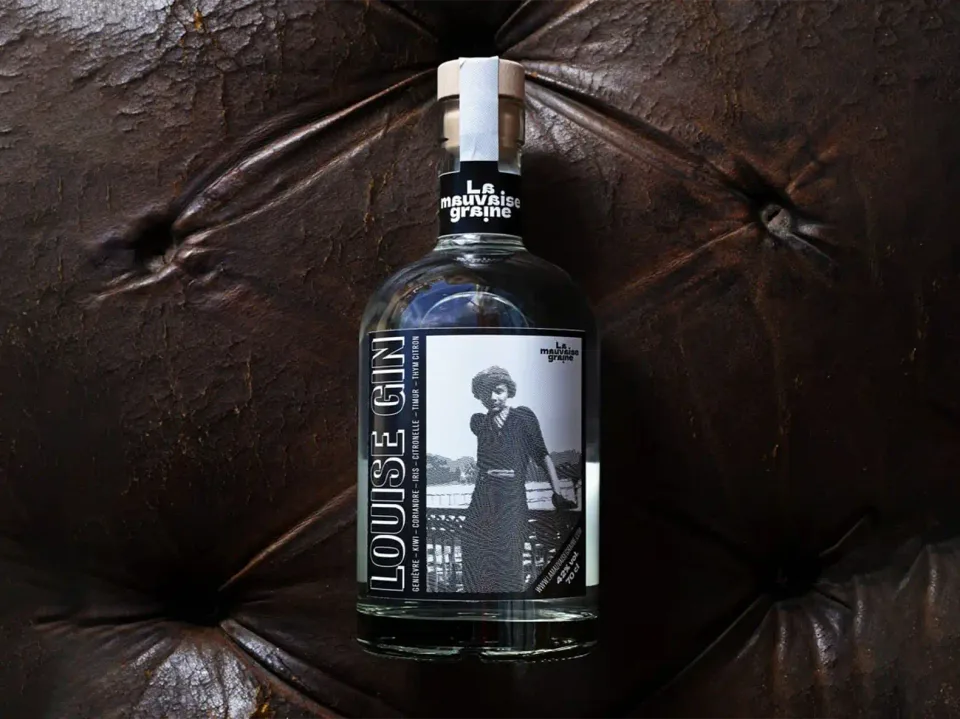
A good gin does not begin in the glass, but in the decision to carefully choose, understand, and bring together every aroma into a complete whole. In the case of Louise Gin, that path leads through Lyon, modern distillation, and a botanical profile based on freshness, natural ingredients, and precise work in the still.
La Mauvaise Graine Distillerie produces its signature gin in the heart of Lyon, on a modern DES column still. Their Louise Gin stands out with a kiwi tincture from the Drôme region and a combination of six botanicals sourced from organic farming or wild harvesting.
Recently, this gin won a gold medal at the Concours International de Lyon, making the recognition even more symbolic. A product created in Lyon was awarded in its own city, in front of an expert environment that truly understands aroma, craft, and quality.
Gin that begins with character
La Mauvaise Graine is not a distillery that wants to make a generic gin. Their Louise Gin has a clearly defined identity and aromatic direction.
On the distillery’s official website, it is stated that Louise Gin is distilled in a column alembic in the heart of Lyon. Its distinctive character comes from a tincture of kiwi grown in the Drôme region, combined with six other botanicals sourced from organic farming or wild harvesting.
That immediately says a great deal about their approach. Here, gin is not just an alcohol base with added aromas. It is designed as a product with geography, an idea, and a clear sensory signature.
The fruitiness of kiwi brings roundness.
The botanicals provide depth.
A light bitterness and spicy finish create a character that lasts.
Lyon as the place of origin
The special value of this story lies in the fact that Louise Gin was not created far away from the audience it speaks to. It is produced in Lyon, a city known for gastronomy, a strong culture of taste, and deep respect for craft.
That is why the gold medal won at the Concours International de Lyon carries additional weight. It is not just another award. It is a confirmation of quality in both a local and international context, before an audience and expert environment that truly understands drinks, aroma, and production.
For a young or signature distillery, such recognition means a great deal. It confirms that the product is not interesting only because of its idea, but also because of the quality in the glass.
The DES still as part of the process
For gin production, especially gin based on carefully selected botanicals, equipment plays an extremely important role. A good still must enable process control, stable distillation, and precise extraction of aromatic components.
La Mauvaise Graine produces its Louise Gin on a modern DES column still. This type of equipment gives the distiller the ability to work with complex aromatic profiles, preserve the delicate notes of herbs and fruit, and achieve a clean, balanced, and repeatable result.
In gin, balance is crucial.
If the alcohol base is too harsh, the botanicals lose their elegance.
If the aromas are overemphasized, the product becomes heavy.
If the distillation is imprecise, what makes the gin recognizable is lost.
A high-quality still does not create the recipe instead of the distiller, but it gives them the control to carry out their idea exactly as they imagined it.
When botanicals have space to speak
Louise Gin is a good example of a modern approach to gin. Instead of relying only on the classic image of gin, it builds its identity through an unusual choice of botanicals and a fruit component that makes it stand out.
Kiwi from the Drôme region is not a detail added for exotic appeal. It gives the product roundness, freshness, and a different aromatic opening. Combined with botanicals from organic farming and wild harvesting, it creates a gin with a natural yet modern character.
This is what more and more modern distilleries are looking for: a product with a craft foundation, a local story, and a recognizable taste.
DES stills are made precisely for such producers, for those who want not only stable production, but also the freedom to develop their own style.
What does this story mean for future distillers?
The story of La Mauvaise Graine Distillerie shows how important it is for equipment to match the producer’s ambition.
If you want to produce gin, it is not enough to have only a good list of botanicals. It is necessary to understand how aromas behave during distillation, how balance develops, and how the result is repeated from batch to batch.
Modern column stills enable better process control, more precise work with aromas, and greater production stability. This is especially important for premium gins, where quality is measured not only by the strength of flavor, but also by purity, elegance, and finish.
DES stills are used around the world for the production of brandy, gin, absinthe, liqueurs, vodka, rum, whisky, and other alcoholic spirits. Our range includes more than 40 still models, different types of columns, several heating options, and the possibility of custom production according to production needs.
For distilleries that want to create products with character, the right still is not just a technical part of production. It is a tool that helps an idea become a recognizable brand.
Gold for a gin that carries its city
La Mauvaise Graine Distillerie shows how a modern urban distillery can combine local identity, creativity, and a serious approach to production.
From the heart of Lyon came Louise Gin, a gin with the aromatic signature of kiwi, carefully selected botanicals, and a character recognized with a gold medal at the Concours International de Lyon.
For DES, it is a special honor that our modern column still is part of this story.
Because when a distiller has a clear idea, high-quality ingredients, and equipment that enables precise distillation, the result is not just a good gin.
The result is a product with a voice, origin, and character.
Contact us and find the DES still that suits your production.